 AESAAportaciones Especiales
04 / Plasma Transferred Arc
PTA cladding for industrial manufacturing and repair
PTA cladding selected to suit the component material and service requirements.
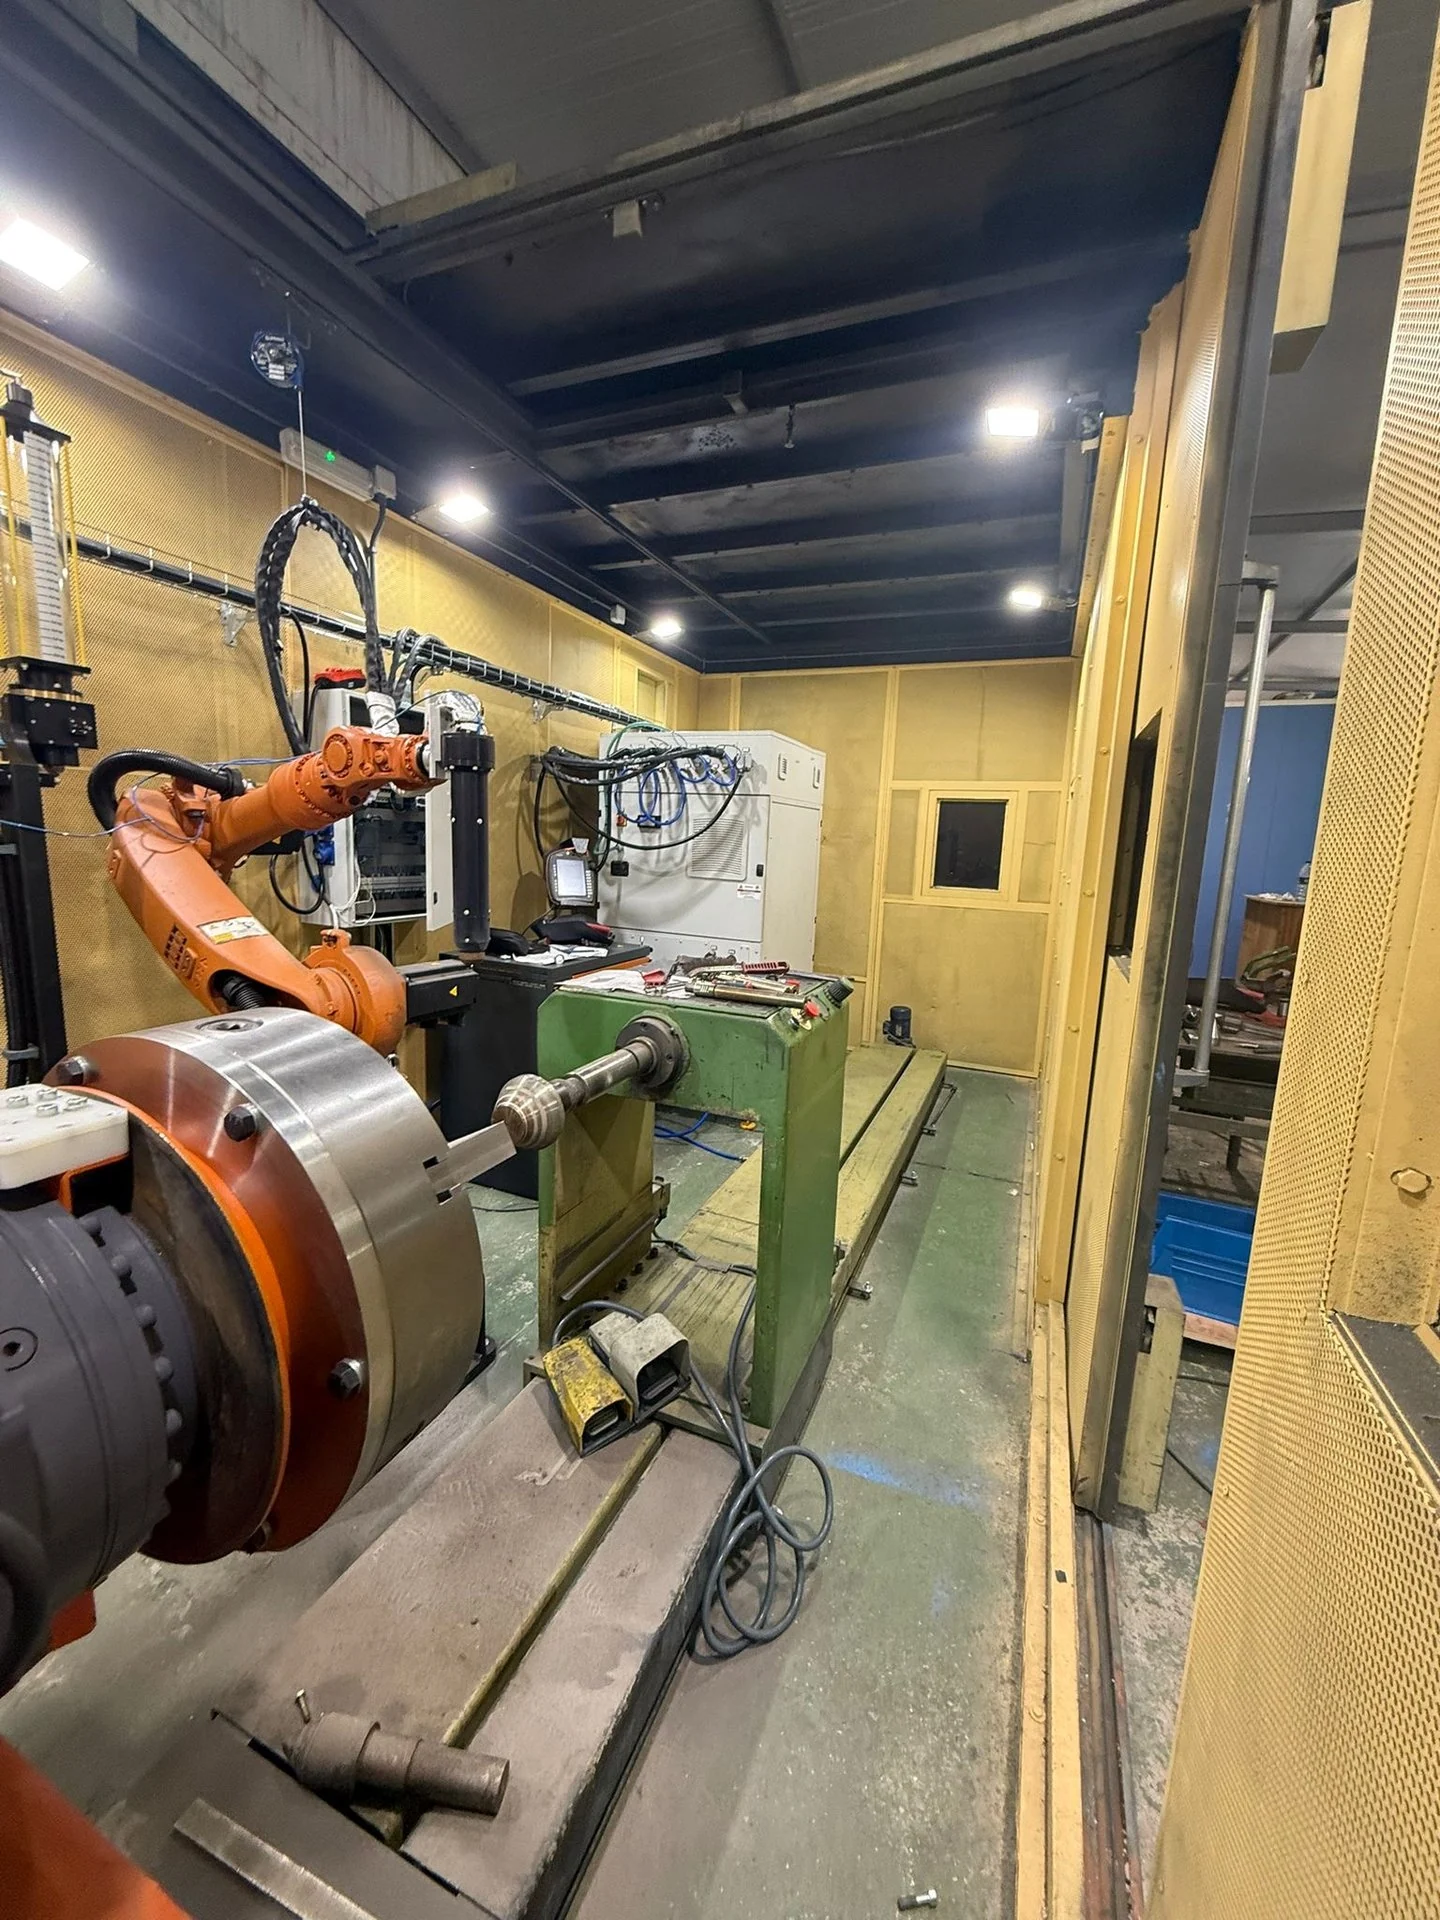
Request a Quote ↗PTA (Plasma Transferred Arc) welding concentrates a plasma arc on the surface while feeding the cladding material into the arc. The process creates a metallurgical bond with the component. AESA uses PTA on new and repaired components where the surface requires a different composition or performance from the base material.
Technical information
PTA
Applications and process selection
Selection starts with the substrate, required surface behaviour and service conditions. Cladding is coordinated with machining, grinding and inspection to establish the final component condition.
Geometry, torch access and the component’s thermal response must be assessed before selecting PTA. Laser cladding provides another fusion-deposition option; HVOF and APS are compared where the surface function calls for a sprayed layer. Selection follows component requirements and evidence for the coating system.
Component dimensions and head access
- Maximum component length
- 2000 mm
- Maximum component diameter
- Ø 800 mm
- Minimum bore diameter for head access
- Ø 100 mm
- Approximate internal deposition reach
- Approximately 300 mm
Feasibility is reviewed against component geometry, workholding, surface access and job requirements. Maximum length and diameter do not establish feasibility for every combination. Head-access diameters are not finished bore dimensions.
Representative materials
- Stellite 1, 6 and 12
- Inconel 625
- Tungsten 60/40: 60% tungsten and 40% nickel-based matrix
- Ultimate
- Colmonoy 4, 5 and 6 · by PTA
Coating selection and applications
- Stellite grades are selected for wear, metal-to-metal sliding and galling resistance. Typical applications include valve seats and contact surfaces; impact loading and service temperature also influence grade selection.
- Inconel is considered when corrosion resistance is the priority. Grade selection requires details of the process fluid, temperature and final deposit chemistry, which can be affected by dilution from the substrate.
- AESA applies Colmonoy grades by PTA. These nickel-based alloys are selected for wear and corrosion resistance, balancing hardness, impact resistance and finishing requirements. Typical applications include sleeves, plungers and wear rings.
- Nickel-based tungsten 60/40 is considered for surfaces exposed to abrasion. Selection requires review of the powder data sheet and loading conditions. Recommendations for Ultimate depend on the specific product reference and its technical data sheet.
- PTA is considered for fusion-bonded metallic overlays on new components or for restoring worn surfaces. Geometry, torch access and the component’s response to heat are assessed before choosing between PTA and laser cladding.
- Selection guidance: material, thickness, preparation and inspection requirements are confirmed for each component. Cladding alloy families cannot be substituted without reviewing the service conditions.
Capacity and applications
- Cladding on new components to achieve the required surface properties
- Repair of high-value industrial components
Technical enquiries
Frequently asked questions
What does PTA stand for?
Plasma Transferred Arc. It is a fusion-cladding process used by AESA with robotised equipment.
Which materials do you apply by PTA?
AESA uses Stellite 1, 6 and 12, Inconel 625 and Colmonoy 4, 5 and 6 by PTA, alongside nickel-based tungsten 60/40 and Ultimate. Selection requires review of the application and feedstock data.
Does AESA offer Colmonoy through other processes?
AESA’s confirmed Colmonoy service uses PTA. This describes AESA’s offering, not a general restriction applying to every commercial grade.
Do you accept one-off components?
Yes. AESA accepts one-off components. Feasibility and scope are assessed against the component and its requirements.
How soon will you respond to an RFQ?
Our usual RFQ response time is three working days. Manufacturing or repair lead time is established in the quotation.
Do you work with customers outside Spain?
Yes. AESA works internationally. Please include the country of origin, component location and delivery requirements in your enquiry.
What documentation and traceability do you provide?
AESA provides certificates relating to the base material, deposition material and quality control for the job. Our integrated management application identifies the cladding batch applied to each component. Documentation and inspection requirements are reviewed with the order.
What should I include in an RFQ?
Include the component, known material, quantity, dimensions, service conditions and required outcome. Drawings can be sent to aesa@aportaciones-especiales.com. The website form does not support file attachments.